If you’re here because you’re already working with a Shuttle Table HF Welding Machine (or shopping for one, and curious how the heck you make sure the welds it cranks out are actually good—wait till you hear the tricks our team’s picked up over 10 years of supplying these machines), you’re in the right spot. A lot of new operators think “HF welding” is just turn a dial, hit a button, and call it a day. Nah, no way—bad welds here can mean wasted materials, failed parts, or even safety issues if it’s for stuff like vinyl tarps, automotive trim, or inflatable boats. Let’s break down the actual, practical inspection methods we teach every customer, no fancy jargon that makes your eyes glaze over. Shuttle Table HF Welding Machine
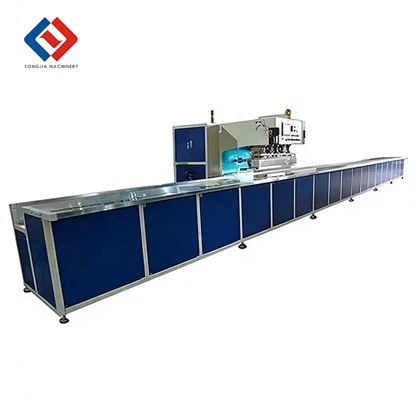
First, let’s set the scene: a Shuttle Table HF machine is that two-table system that slides back and forth super fast—one table’s loading/unloading while the other’s welding, so you’re not standing around waiting. It’s great for high-volume stuff, but the fast shuttle cycle means you can’t just wing inspections; you need a solid, repeatable process.
Start with the most basic, no-equipment check: visual inspection. Wait, not just “look at it”—specifically for HF welds. HF (high frequency) welding melts the material along the seam, so you’re looking for a smooth, even bead, right? No gaps, no blobs, no areas where the material didn’t fuse fully. A common mistake we see is new operators rushing the shuttle cycle, so the heat doesn’t soak all the way through thick materials (like 20 oz vinyl vs. thin 6 oz). So here’s how we do it: after a weld cools for 10-15 seconds (HF welds stay hot for a sec, touching it too soon distorts it), run a gloved finger along the seam. If it feels smooth, no bumps or indentations from bad pressure, that’s a win. If you feel a gap? That’s a red flag. Also, check for “burn through”—tiny holes in the seam, usually from too much power or too long a weld time. We had a customer last month who skipped this and sent a batch of inflatable rafts to a campground, and 30% had pinholes from burn through. Oops. Fix: we add a simple pressure gauge upgrade to our machines now that takes the guesswork out of pressure settings.
Next, the bend test—this is the go-to for our regulars. It’s cheap, fast, and tells you way more than just looking. How? Cut a 1-inch wide strip of your welded part, hold each end, and bend it back and forth 3-4 times along the weld seam. If the weld breaks before the material? That’s bad. If the material tears before the weld? Perfect. Wait, why does that work? Because HF welds should fuse the material’s molecules, not just stick them on top. If it’s a weak bond, the weld cracks easy. We teach customers to do this test on every first part of a new job, right after setting up the machine (new material thickness, new color, even different lots of vinyl can change weld strength). Last week, a guy was welding clear PVC bags for medical supplies, and the bend test failed—turns out he forgot to lower the electrode gap when switching from black vinyl. Fixed that in 2 minutes, no wasted batch. Pro tip: don’t bend it too hard at first; gentle bends first, then crank it a bit. Some thin materials (like 6 oz tarp) will break if you yank, but that’s normal. The key is comparing the weld strength to the base material.
Then there’s the peel test, which is a bit more in-depth, but we use it for critical parts—like truck bed liners or safety mats where a bad weld could cause a hazard. Cut a weld strip that’s 2 inches wide, make a small cut in the seam, then peel the two layers apart slowly. If the peel leaves material tearing along the entire seam (called “adhesive failure” in industrial terms, but we just say “pulling the fabric, not the weld”), that’s solid. If it peels right apart cleanly? No fusion, trash. We used to skip peel tests until a customer had a bunch of boat covers that split in a rainstorm—they thought the visual check was enough, but the weld was only surface-bonded. Now every customer who makes heavy-duty covers or structural parts gets a free peel test demo from our techs when they pick up the machine. Oh, and for multi-layer parts (like a tarp with a mesh core), we do a peel test on each layer to make sure none are separating.
Wait, what about non-destructive tests? Those are for when you can’t ruin the part, right? Like if you’re making a one-of-a-kind custom part, or a batch where every single piece is super valuable. The most common one for HF welds is the ultrasonic test. It sends sound waves through the seam, and if the waves bounce back unevenly, that means there’s a gap or weak spot. We don’t keep ultrasonic testers in stock, but we partner with a local industrial testing company that gives our customers a discount—plus, we add a cheat sheet for how to set the test frequency based on material thickness in every machine manual. Another non-destructive one? The air pressure test, which is perfect for inflatables (boats, bounce houses, air mattresses). You inject a small amount of air into the part, submerge it in water, and look for bubbles. That’s a no-brainer, but a lot of new operators forget to test the seams, not just the whole part. We had a bounce house manufacturer last year who only tested the outer wall, and the welds for the side panels were leaking—cost ’em a whole batch. Now we add a free air test nozzle kit to every Shuttle Table HF machine sale for inflatable jobs.
Now, here’s the part no one talks about: pre-production checks that prevent bad welds before you even hit the “start” button. Because inspection is only half the battle—stopping bad welds from happening is better. First, check your material. Some plastics (like PE) don’t weld well with HF, so we make sure every customer gets a quick material compatibility guide when they buy a machine. We also calibrate our machines before shipping, but operators should double-check the electrode alignment once a week—if one electrode is off-center, you’ll get a lopsided weld. Last month, a customer’s machine had a misaligned upper electrode, so half the seam was weak. He did a visual check on the first part, caught it, and didn’t waste 500 yards of vinyl. That’s the thing—these machines are reliable, but they still need tiny checks.
Wait, what about common pitfalls with Shuttle Table models specifically? Because they shuttle back and forth, sometimes the timing of the weld cycle gets off. Like, if the table moves before the weld is fully cured, the seam will separate. So we tell customers to set a 2-second “hold time” after the weld power cuts out, so the material cools and fuses before the table slides. That’s a setting you can adjust in 30 seconds, but so many new operators miss it. We even have a little sticker on the machine’s control panel that says “WELD HOLD TIME = MANDATORY” to remind people. Another shuttle-specific issue: clamp pressure. The two tables need to clamp the material evenly along the entire seam—if one end is loose, you’ll get a weak spot. We add pressure sensors to all our Shuttle Table HF machines now that alert the operator if pressure drops below a set level, so they catch that mid-job, not after a whole batch is bad.
Let’s wrap this up with a real example from our shop. Last quarter, we supplied a Shuttle Table HF machine to a manufacturer of automotive sun visors. They were having issues with welds failing the bend test—so we sent one of our techs out. He ran a visual check on their first part, saw a tiny indentation in the seam, checked the electrode gap, and found it was set too wide for the 0.02 inch PVC they were using. He adjusted the gap, did a bend test, passed, and they’ve been running 1,000 visors a day without a single failed weld. That’s exactly why we focus on these inspection methods—they’re practical, not just textbook stuff.
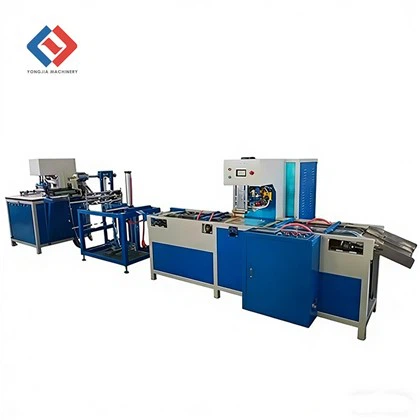
If you’re in the market for a Shuttle Table HF Welding Machine, or you’re having issues with your current one’s weld quality, don’t guess. We’ve been working with these machines for years, and we can walk you through every step—from setup to inspection to fixing little quirks that cause bad welds. We’re not salespeople who just push machines; we’re the guys who built, tested, and fixed these things for hundreds of customers over the years. Hit us up, and we’ll chat through your specific needs—whether you’re welding small parts or big heavy stuff, we can make sure you get the machine that fits, and the inspection processes to keep your parts consistent.
Plastic Bag Making Machine References
- Industrial Welding Association. HF Welding Best Practices for Thermoplastic Materials. 2022
- Shuttle Table Machine Operators Guide, Heavy Duty Equipment Corp. 2023
- Non-Destructive Testing for Plastic Welds, Journal of Industrial Manufacturing. Vol. 18, No. 4, 2021
Dongguan Yongjia Machinery Equipment Co., Ltd.
We are one of the most reliable shuttle table hf welding machine manufacturers and suppliers in China, specialized in providing high quality customized service. Please feel free to wholesale advanced shuttle table hf welding machine at low price from our factory. For quotation, contact us now.
Address: No. 240, Chashan South Road, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: info@yjwelding.com
WebSite: https://www.yjhighfrequencymachine.com/
